
THT Auto Insertion Solutions: AI-6188, AI-6288 & AI-6488 Inserters
A product-family overview of the AI-series THT inserters — the AI-6188 radial, AI-6288 axial, and AI-6488 jumper-wire models — and how to match each one to your board mix.
Aug 11, 2026 · Updated Aug 31, 2026 · Jason Wu
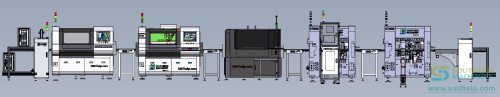
THT Auto Insertion Solutions: AI-6188, AI-6288 & AI-6488 Inserters
Through-hole insertion is often the last heavily manual step on a PCB assembly line. A mixed component set makes it even harder: axial resistors, radial capacitors, LEDs, transistors, and jumper wires each require different handling. Southern Machinery’s AI-series THT auto insertion solutions — the AI-6188 radial inserter, AI-6288 axial inserter, and AI-6488 jumper-wire inserter — replace repetitive handwork with servo-driven, PC-controlled automation at up to 0.4 seconds per component.
The cost you haven't named: mixed THT component handling
A mixed through-hole bill of materials exposes the limits of manual insertion.
- Multiple handling methods. Axial, radial, and jumper parts each require a different insertion motion, so one operator can’t move efficiently across the whole board.
- Pace and fatigue. Manual insertion speed varies by shift and experience, leading to uneven output and defects.
- Labor cost per board. Every lead placed by hand adds direct labor that scales poorly with volume.
- Scaling limits. More volume means hiring more people, not just running more machine time.
- Program spread. Each part family often runs on a different bench with its own setup sheet. A board mixing axial, radial, and jumper work has to cross three work areas — and three chances for a mis-setup.
The Three-Machine THT Insertion Plan
Match each component family to the right machine before buying. Think of it as the Three-Machine THT Insertion Plan.
- Classify your component mix. Sort your through-hole parts into axial, radial, and jumper-wire families, plus any odd-form exceptions, so each gets the correct insertion method.
- Match each family to a machine. Assign axial parts to the AI-6288, radial parts to the AI-6188, and jumper wires to the AI-6488. These three cover the bulk of a typical board.
- Sequence the line. Arrange the machines to follow the board’s insertion logic, with loading and unloading between stations, so the board flows without manual carries.
- Confirm the shared data. Define what each machine reports and how they hand off, so the family runs as one coordinated process rather than isolated cells.

The vehicle: the AI-series inserter family
The framework maps onto the three core machines.
- Classify the mix → the right machine per part. The AI-6288 handles axial resistors and diodes; the AI-6188 covers radial capacitors, LEDs, and transistors; the AI-6488 places jumper wires.
- Match the family → proven speed. Each machine runs at around 0.4 s per component, giving consistent throughput across different part types.
- Sequence the line → connected flow. With automatic PCB loading and unloading options, the machines form a continuous insertion stage instead of separate benches.
- Confirm the data → coordinated cells. Shared program and status reporting let the family run as one line under a single operator overview.
Specification note: confirm component-type range, feeder capacity, and loading options at quotation, because they depend on your board’s part mix and volume.
Across an existing line, the three inserters share one PC-controlled cell layout. A board moves from the AI-6288 axial stage to the AI-6188 radial stage, then the AI-6488 jumper stage, without leaving the conveyor. Their program and status data travel on the same bus to the line MES, so one operator sees feeder counts and faults for all three machines on a single screen.

Specifications
| Machine | Role | Speed |
| --- | --- | --- |
| AI-6288 | Axial component inserter | 0.4 s / piece |
| AI-6188 | Radial component inserter | 0.4 s / piece (typical) |
| AI-6488 | Jumper-wire inserter | 0.4 s / piece (typical) |
| Component types (AI-6288) | 40 – 160 types | Per configuration |
| Board handling | Automatic load / unload options | Per line layout |
| Control | PC-controlled, servo-driven | — |
| Typical parts | Resistors, diodes, capacitors, LEDs, transistors, jumpers | — |
| Operator model | One overview across machines | Per layout |
The loop: re-balance when the mix shifts
Product mixes change, and a line tuned for one board can choke on the next. Build a loop: every time a new product enters, re-run the Three-Machine THT Insertion Plan, check the axial/radial/jumper split, and re-balance machine assignment and feeders with your process team. Review throughput logs monthly. Treat the family mapping as a living plan — the loop is what keeps all three machines loaded evenly instead of one starving while another waits.
Your next step
Send us your through-hole component list by family. We will return a machine-matching outline showing which AI-series inserter fits each part type, estimated throughput, and what to confirm at quotation. Reach Jason at jasonwu@smthelp.com or on WhatsApp +86 13602562576.
FAQ
What does each AI-series machine do?
AI-6288 inserts axial parts, AI-6188 inserts radial parts, and AI-6488 inserts jumper wires.
How fast are they?
Around 0.4 seconds per component; actual rate depends on board and program.
Can they run together as a line?
Yes, with automatic loading and unloading options they form a connected insertion stage.
Do they handle odd-form parts?
Odd-form parts are covered by other Southern Machinery solutions; the AI series targets axial, radial, and jumper families.
What should I send to start?
Your through-hole component list grouped by axial, radial, and jumper families.
Jason Wu
Founder & CEO, Southern Machinery (Shenzhen Southern Machinery Sales and Service Co., Ltd.)
Email: jasonwu@smthelp.com / info@smthelp.com
WhatsApp: +86 13602562576
Catalog & manuals: file.autoinsertion.com | Machine photos: ph.smthelp.com
LinkedIn: linkedin.com/in/smtsupplier | YouTube: youtube.com/c/Smthelping
Comments
Comments appear after approval.